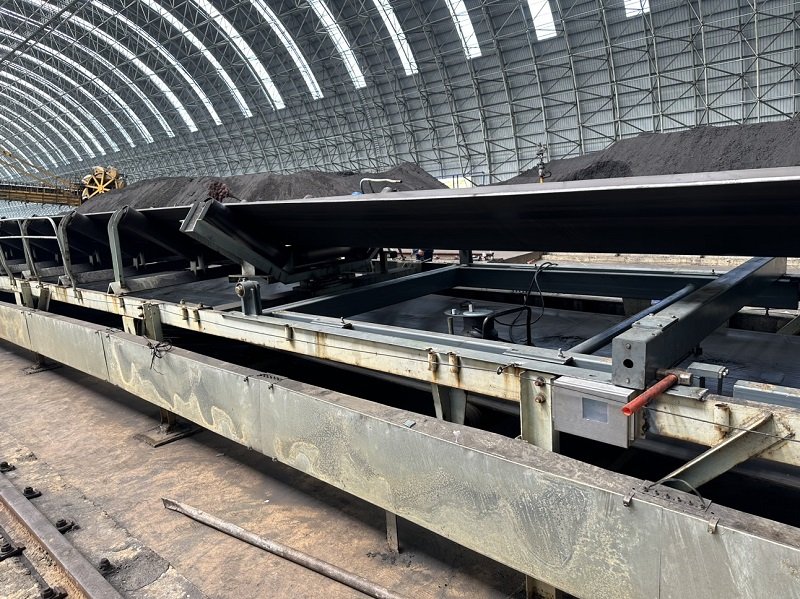
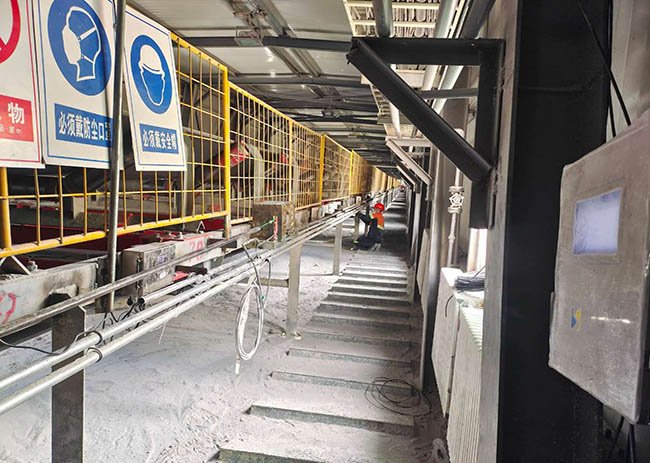
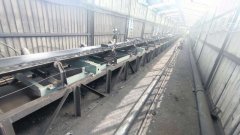
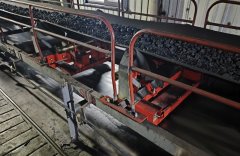
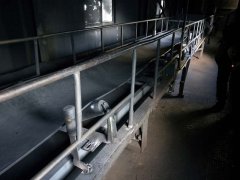
At depths of hundreds of meters underground in coal mines, conveyor belts operate day and night, continuously transporting raw coal from the mining face to the surface. In this vast transportation network, mining explosion-proof belt scales are widely used as weighing equipment. However, with the deepening of intelligent mining construction, the role of explosion-proof belt scales is being redefined: it is no longer just about weighing, but has grown into an intelligent control core node that runs through the entire chain of coal mine safety, production, management, and decision-making.
Traditional coal mine material control has long had many industry pain points. In the past, most small and medium-sized coal mines relied on manual ledger statistics and offline weighing verification to calculate raw coal production, which was not only time-consuming and inefficient, but also prone to errors, omissions, and mistakes in manual operations, resulting in distorted production capacity data.
At the same time, underground dust concentration is high, humidity is high, and there are flammable and explosive gases present. Ordinary weighing equipment cannot adapt to the special working conditions underground, which can easily lead to equipment failures, inaccurate measurements, safety hazards, and other problems.
More importantly, traditional weighing equipment can only achieve single data statistics and cannot be integrated with intelligent control systems. Production data is outdated and fragmented, making it difficult for management to grasp underground transportation capacity and equipment operation status in real time, and unable to accurately control production rhythm, which restricts the intelligent and standardized development of coal mines.
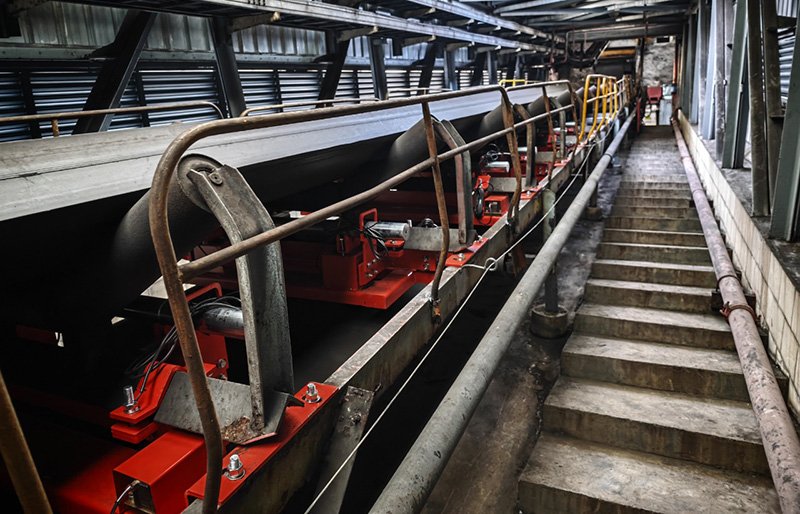
The practical application of mining explosion-proof belt scales has completely broken the functional limitations of traditional weighing equipment, achieving a leapfrog upgrade from "single measurement" to "intelligent control". Firstly, the core advantage of the equipment lies in its adaptability to mining explosion-proof requirements. It strictly follows the explosion-proof standards for coal mines and is designed to be dust-proof, moisture-proof, and corrosion-resistant. It can operate stably in complex underground conditions with high dust, high gas, and humidity, eliminating electrical safety hazards at the hardware level. It conforms to the hard regulations for coal mine safety production and builds a solid defense line for underground production safety.
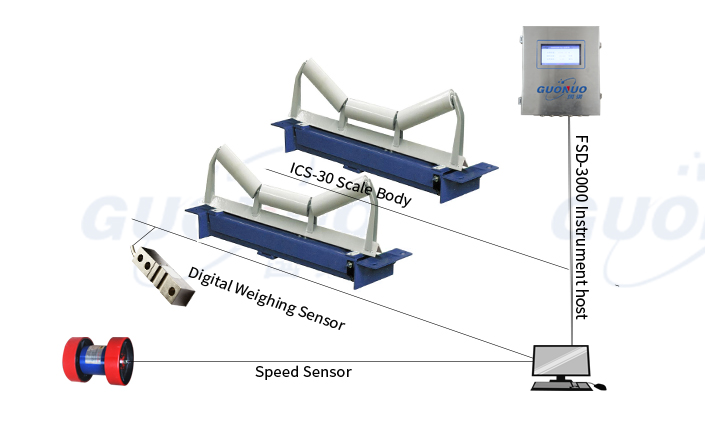
Secondly, its core value lies in dynamic and accurate data collection and real-time transmission. The mining explosion-proof belt scale can monitor core data such as raw coal flow rate, cumulative production, and conveying speed in real time during the belt conveying process, with millisecond level collection and real-time synchronization.
The measurement accuracy is stable and controllable, effectively avoiding manual statistical errors. More importantly, the equipment can seamlessly integrate with the coal mine intelligent control platform and big data scheduling system, uploading real-time underground material transportation data to the cloud, realizing the visualization, digitization, and traceability of underground production data, and enabling coal mine production to break away from "experiential management" and enter a new stage of "data-driven control".
In actual coal mine production and operation, the intelligent control value of mining explosion-proof belt scales is reflected in multiple core scenarios. In terms of capacity control, the system can real-time calculate daily, monthly, and annual raw coal production, automatically generate production reports, without the need for manual summary and accounting, greatly improving the efficiency and accuracy of capacity statistics, and providing accurate data basis for production planning, capacity assessment, and resource allocation.
In terms of equipment operation and maintenance, by monitoring fluctuations in material conveying flow and belt operating load data, it is possible to accurately identify potential faults such as belt conveyor overload, no-load, and abnormal jamming, improve equipment operation and maintenance efficiency, reduce equipment downtime due to faults, and enhance the stability of the conveying system operation.
At the same time, this equipment also plays an important role in safety compliance and energy conservation. Accurate material measurement data can assist coal mines in achieving precise production allocation and scheduling, avoiding problems such as ineffective conveying and overloaded operation, reducing equipment energy consumption and belt wear, and reducing operation and maintenance costs. In addition, complete, authentic, and traceable production data can provide data support for coal mine safety inspections, capacity checks, compliance audits, and other work, helping coal mines achieve standardized and regulated production.
Nowadays, the intelligent construction of coal mines has entered a critical stage of deep cultivation and meticulous work, and every underground intelligent device is an important antenna of the control system. The mining explosion-proof belt scale is no longer a simple auxiliary weighing device, but a core data node that connects underground transportation, production statistics, equipment operation and maintenance, and safety control, breaking down the data barriers between coal mine material production and intelligent control.